Top 15 Features of QBY Air Operated Diaphragm Pump – Why Choose AODD Technology
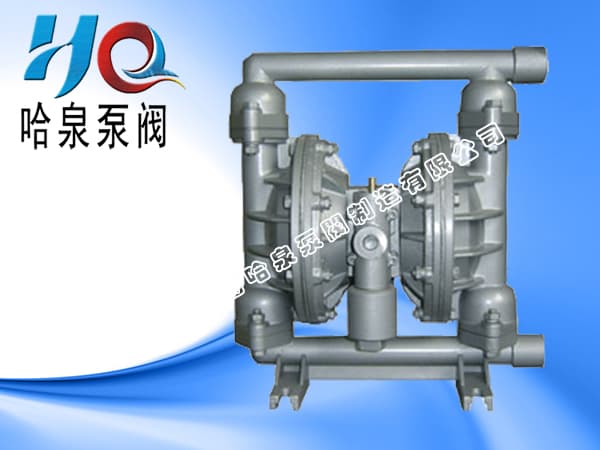
The QBY series pneumatic diaphragm pump offers numerous advantages over traditional centrifugal and electric pumps. First, it does not overheat during operation because compressed air expands and absorbs heat as it exhausts, naturally cooling the pump. Second, there is no motor or electrical part at the pump, which is why it is often chosen for flammable liquids. Third, the pump can handle liquids containing solid particles up to 10 mm in diameter thanks to its positive displacement design and ball valve inlet.
Fourth, the pump generates extremely low shear forces on the pumped media. Materials enter and exit the pump with minimal agitation, making it ideal for shear-sensitive substances like food emulsions, biological cultures, and unstable chemicals. Fifth, flow rate is fully adjustable by adding a throttling valve at the outlet or varying the air supply pressure. Sixth, the pump has excellent self-priming capability and can lift liquid from depths of 5 to 7 meters without any foot valve or priming chamber.
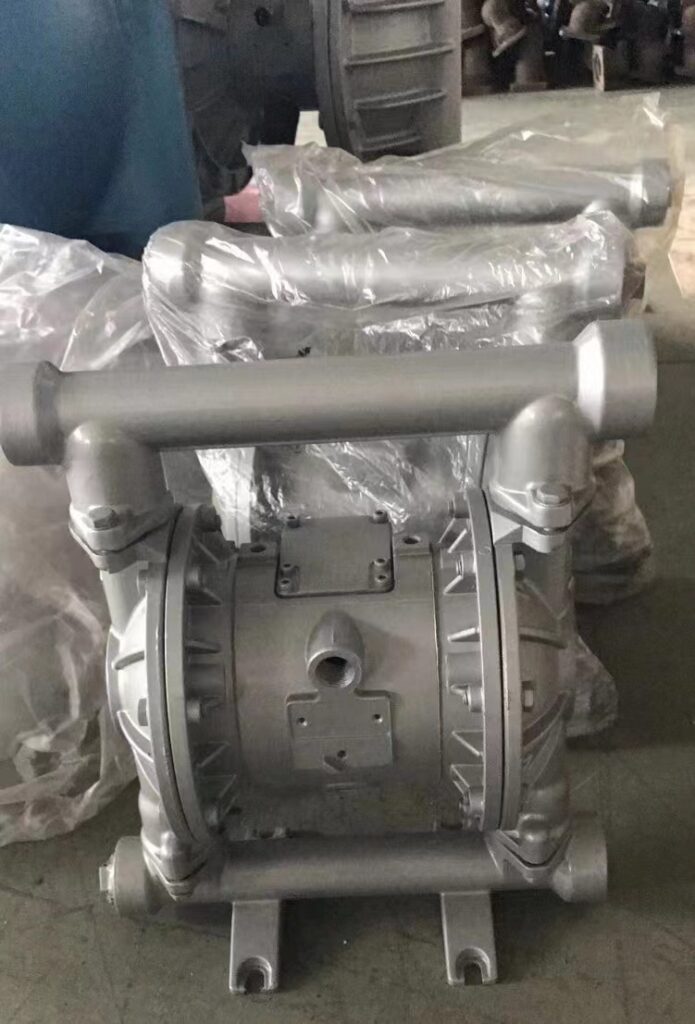
Additional benefits include the ability to run dry indefinitely without damage, fully submersible operation, and compatibility with an extremely wide range of fluids from low-viscosity solvents to high-viscosity pastes exceeding 10,000 centipoise. The pump has no complex control systems, no cables or fuses, and is lightweight and portable. It requires no lubrication, reducing maintenance and eliminating drips that could contaminate the work environment. The pump maintains high efficiency throughout its service life and automatically stops when the outlet is closed, preventing energy waste.
Products in This Series
 QBY Air-Operated Diaphragm Pump (AODD)
1 Inch Electric Diaphragm Pump, 3 m³/h at 40 m, with PTFE-Family Diaphragms
A 1 inch electric diaphragm pump for 3 m³/h at 40 m head, with F46 diaphragms and a plastic or stainless steel body. When to choose electric over air.
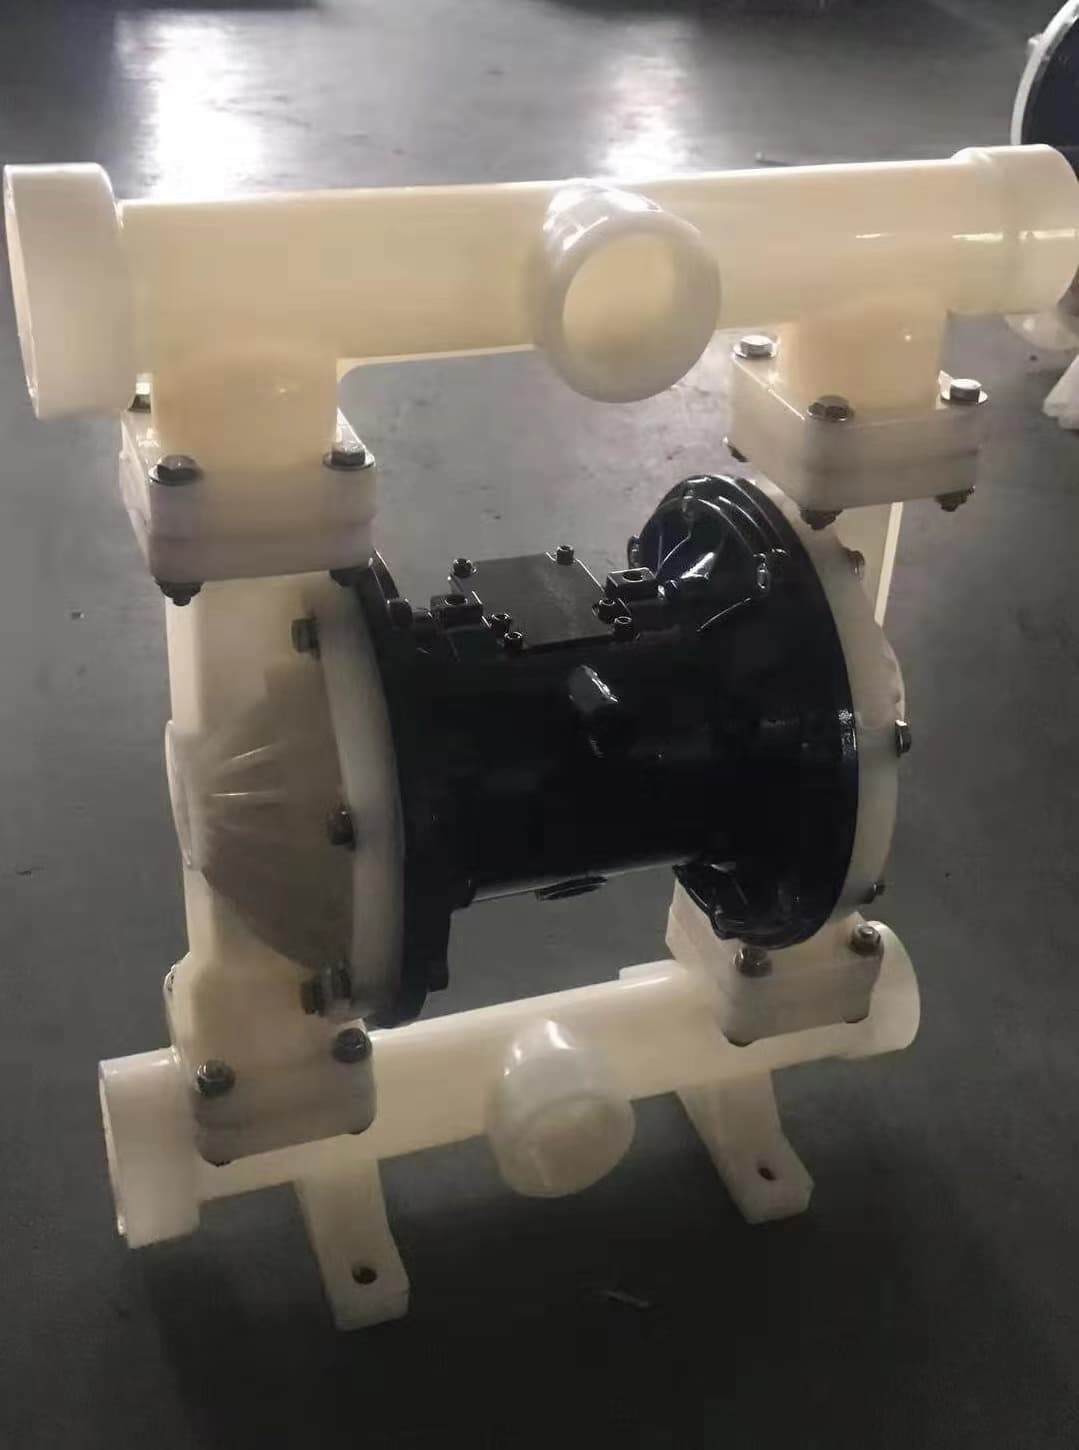 QBY Air-Operated Diaphragm Pump (AODD)
Polypropylene QBY5 Diaphragm Pumps for Acid Transfer: 1/2 and 2 Inch
Polypropylene QBY5 air diaphragm pumps for acids, in 1/2 inch and 2 inch (QBY5-50) sizes: what each size delivers and what to check before ordering.
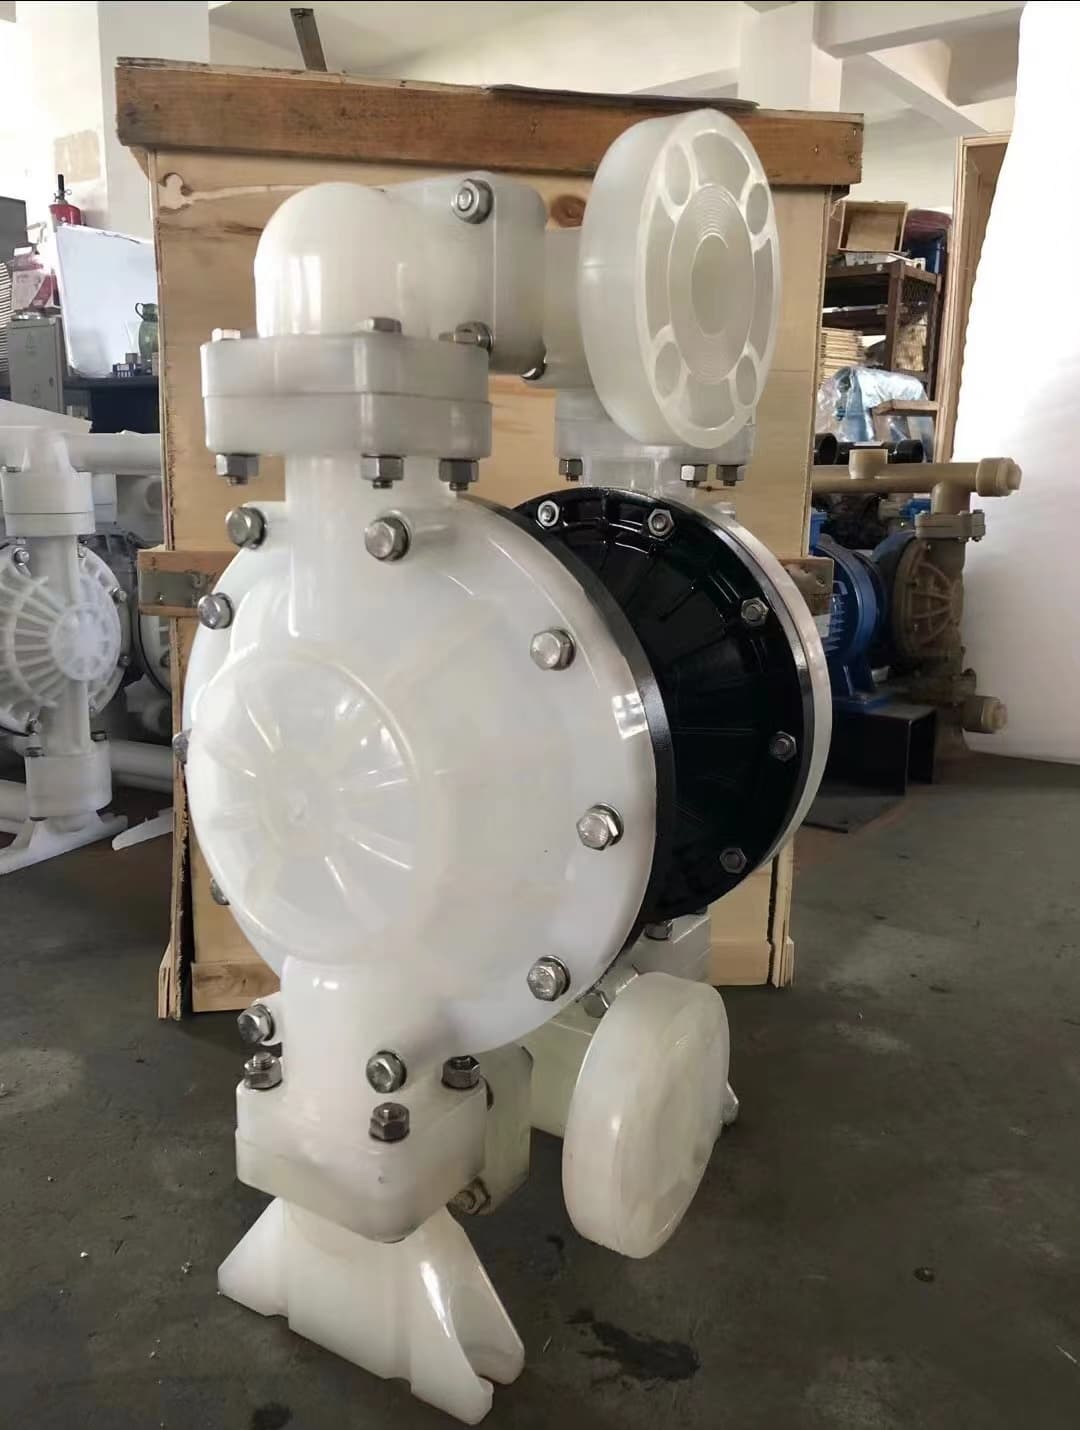 QBY Air-Operated Diaphragm Pump (AODD)
QBY Diaphragm Pump Weight, Packing and Lead Time
How much does a QBY air diaphragm pump weigh, how is it packed, and how fast can it ship? Real figures from our orders, plus the spares to order with it.
Need a pump for your application?
Our engineers respond to technical inquiries within 24 hours.
Get a Quote